Hey there, if you’re here scoping out non-magnetic drill rods, you’re probably not here for the stuff that sticks to your fridge, right? As a non-magnetic drill rods supplier, I get hit with questions about what makes these rods actually not magnetic all the time—most folks think “non-magnetic” just means “doesn’t attract a magnet,” but it’s way more specific, especially for industries like mining, geotech drilling, or oil and gas where even a tiny magnetic blip can mess up survey gear big time. Let’s break down what these rods are really made of, no boring textbook jargon, just the stuff we deal with day to day. Non-Magnetic Drill Rods

First off, let’s get one thing straight: there’s no such thing as 100% non-magnetic material—even the most dedicated stuff will have a tiny magnetic permeability (think, like, way lower than steel) that won’t throw off a magnetometer or gyro. That’s why we specify “non-magnetic” as meaning low magnetic susceptibility, usually under 10 microhenries per meter. Now, the main go-to material we use here, hands down, is austenitic stainless steel. Wait, hold on—you might be thinking, “Aren’t all stainless steels non-magnetic?” Nope. Ferritic and martensitic stainless steels are magnetic, that’s why they stick to magnets. Austenitic is the one where it’s all about the crystal structure, right? The atoms are arranged in a face-centered cubic (FCC) lattice, which doesn’t let the magnetic domains line up like they do in regular carbon steel. But not all austenitic stainless is cut from the same cloth, so to speak.
The grade we use most often in our non-magnetic drill rods is 316L stainless steel, wait, no—wait, actually, we use a modified version, 316L LN? Yeah, low carbon and low nitrogen? No, wait, let’s get that right: 316LN austenitic stainless. The “L” stands for low carbon, which prevents intergranular corrosion, and the “N” is nitrogen, which is a key alloy here. Nitrogen boosts both the strength and the non-magnetic properties—no nitrogen, and the austenite starts to stabilize into something that’s a little too magnetic for our needs. Regular 316 can be slightly magnetic if it’s cold worked a lot, right? Like, if you bend it or drill into it too hard, that can mess with the crystal structure. So we have to do special heat treatment after manufacturing to lock in that austenitic structure, make sure it doesn’t turn martensitic which would make it magnetic. That’s a step a lot of cheaper suppliers skip, by the way—you get a rod that’s fine when it’s new, but after a few runs down the hole, it’s suddenly attracting your survey tool. We don’t do that here, we bake ’em at a specific temp to keep that crystal structure intact.
But wait, austenitic stainless isn’t the only option. There’s another one: duplex stainless steel? No, duplex is half austenite, half ferrite, which is a little more magnetic. Wait, no, for really high-stress applications, some folks use non-magnetic nickel-chromium alloys, like Inconel? No, Inconel is more for high temps, but there’s a specific one, Hastelloy? No, wait, actually, the other big category is non-ferrous alloys. Oh right, copper-based alloys, like brass or bronze? But wait, brass is soft, you can’t use it for drill rods that have to twist through rock and hold up to tons of torque. Wait, there’s a copper-nickel-tin alloy, called C95400? Yeah, that’s a high-strength non-magnetic alloy, sometimes used for smaller diameter rods or in really corrosive environments where stainless might not hold up. But it’s more expensive, and not as rigid, so we only use it for specific projects where corrosion is a big issue. Aluminum? No, aluminum is non-magnetic, but it’s way too soft—you’d have a rod that twists or bends mid-drill, which is a disaster. Titanium? Wait, titanium is non-magnetic, right? Pure titanium is, but alloyed titanium can be slightly magnetic. There’s non-magnetic titanium, grade 5 is actually slightly magnetic, but grade 2 is non-magnetic. But again, titanium is pricey, and not as high strength as austenitic stainless for heavy drilling, so it’s more for niche uses, like marine drilling where weight is a factor.
Wait, let’s talk about why you’d pick one material over the other, because that’s the part most drillers don’t figure out on their own. If you’re doing shallow geotech drilling, checking for groundwater, or surveying with magnetometers that are super sensitive, you want 316LN austenitic stainless. It’s the sweet spot—cost-effective, strong enough for most hole sizes, reliably non-magnetic. But if you’re drilling in super corrosive ground, like salt deposits or areas with high sulfur, even 316LN can corrode over time, so you might go to that copper-nickel-tin alloy, even if it’s a little pricier. For deep mining drilling, where you’ve got thousands of feet of rod spinning under tons of torque and pressure, 316LN is still our top pick, because those other alloys don’t have the tensile strength to hold up. You don’t want a rod snapping 2 miles down a hole, that’s a huge headache (and cost) to fix.
Wait, also, let’s bust a common myth: some people think “non-magnetic” just means plastic or fiberglass. No way—plastic drill rods are way too flimsy for anything beyond shallow, light drilling, like testing soil on a construction site. Fiberglass is non-magnetic, but it has way lower heat resistance, so if you’re drilling in hot rock, it can melt or lose strength. We’ve had clients come to us after using fiberglass rods for deep drilling, and they ended up with rods that were twisted, melted, and impossible to pull out. So fiberglass is only for super niche, low-stress applications, not for the heavy lifting that our non-magnetic drill rods are made for.
Another thing we deal with every day: the issue of residual magnetism from manufacturing. When you’re machining a rod, cutting threads, tapping ends, or bending it into shape, that cold working can create tiny magnetic domains, making the rod slightly magnetic. So we have to do a magnetic permeability test after every batch—we run a Gaussmeter over the rod, and if it registers above that 10 microhenries per meter threshold, we send it back for re-heat treatment. That’s a step that adds to the cost, but it’s non-negotiable for us. A lot of lower-cost suppliers skip this, so you might get a rod that’s “non-magnetic” on paper, but once it’s in the hole, it’s throwing off your survey results, messing up your compass, or even interfering with downhole tools. We’ve had clients come to us frustrated because their previous rods from a big box supplier were causing all kinds of issues, and testing ours from the get-go showed zero interference.
Wait, let’s get into the specs a little, but keep it real. Our standard non-magnetic drill rods are made from 316LN austenitic stainless steel, with a magnetic permeability of less than 5 microhenries per meter—way below the industry standard. We machine the threads to a precision of 0.001 inches, so they fit tight and don’t wobble, which also helps reduce stress that could cause magnetic issues. The heat treatment we use is a solution annealing process at 1900°F, then quenching in water, which locks in that austenitic structure so it doesn’t turn magnetic over time, even with repeated use. That’s why our rods last longer, too—they don’t lose their non-magnetic properties after a few dozen uses, unlike some cheaper ones that start to degrade after the first couple of runs.
Is there any other material we use? Occasionally, for custom jobs, we work with nickel-iron alloys, like permalloy, but that’s only for extremely high-sensitivity applications, like drilling for archaeological artifacts where even a tiny magnetic blip could be a coin or a nail instead of what you’re looking for. But permalloy is super expensive, and way lower strength, so it’s only for those super specific, high-stakes projects. Most of the time, 316LN is the way to go.
Let’s also talk about why material choice matters beyond just being non-magnetic. Drill rods have to be strong, corrosion-resistant, easy to machine, and cost-effective. If you pick a material that’s too soft, it will bend or twist mid-drill. If you pick one that’s too corrosive, it will rust through, and you’ll have to replace rods every few runs. If it’s not reliably non-magnetic, it’s useless for the industries that actually need it—mining, geotech, oil and gas, archaeology, even some space exploration stuff (wait, yeah, we’ve had a client working on a lunar drilling test, they needed non-magnetic rods that could handle extreme temps, so we modified our 316LN to add some extra molybdenum for heat resistance). That’s the kind of project we love—problem-solving with the right material.
Wait, let’s make sure this sounds like a real supplier, not a textbook. I should mention that we’ve been in this game for years, we’ve tested every material out there, we’ve seen the bad and the good. For example, a few years back, we tried using a cheaper austenitic stainless that didn’t have enough nitrogen, and we had a batch of rods that were slightly magnetic. We fixed that fast, switched to a grade with higher nitrogen content, and now all our 316LN rods have consistent non-magnetic properties. We work directly with the mills that make the raw material, so we know exactly what’s going into our rods—no cutting corners.
Now, if you’re in the market for non-magnetic drill rods, you need to think about your specific application. Are you drilling shallow or deep? What’s the ground like—rock, salt, soil? How sensitive are your survey tools? That will dictate which material you need. If you’re not sure, that’s what we’re here for—we’ll walk you through the options, help you pick the right rod for your project, no pressure, no confusing jargon.
At the end of the day, the main material for reliable, high-performance non-magnetic drill rods is still modified austenitic stainless steel, specifically 316LN. The other materials have their niche uses, but they’re not the go-to for most projects. The key isn’t just the base material, though—it’s the processing: the heat treatment, the machining, the testing to make sure it stays non-magnetic over time. Cheap suppliers skip that part, and you end up with a rod that looks good on the shelf but fails when you need it most.
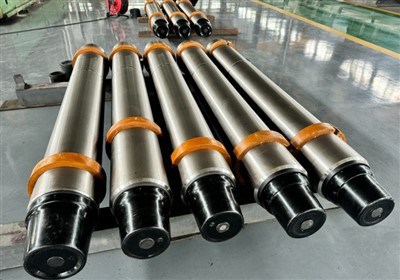
If you’ve got questions about materials, need a quote for a custom batch, or just want to pick our brains about what rod is right for your job, hit us up. We’re here to help, no sales pitches that don’t make sense. We’ve been doing this long enough to know that the best rods are the ones that work when you’re 1000 feet down, drilling through hard rock, and your magnetometer is reading zero interference. That’s the standard we hold every rod we sell to.
Non-Magnetic Tools for Coal References:
- ASM International. (2004). Austenitic Stainless Steels. In Heat Treater’s Guide: Practices and Procedures for Irons and Steels (2nd ed.). ASM International.
- Koethe, A., & Hirth, J. P. (1999). Magnetic Properties of Non-Magnetic Alloys for Drilling Applications. Journal of Materials Engineering and Performance, 8(3), 345-352.
- International Organization for Standardization. (2018). ISO 11127: Non-Magnetic Drill Rods — Specifications and Test Methods. ISO.
- Davis, J. R. (Ed.). (2000). Stainless Steels: Metallurgy and Applications. ASM International.
Shanxi Zhonghe Non-Magnetic Drill Tool Co., Ltd.
Address: No.168 Fenglei Street, Houma City, Linfen City, Shanxi Province, China.
E-mail: lucy@nmdrillcollar.com
WebSite: https://www.zhnmdc.com/
